Call:
 Send Inquiry

 Send Inquiry
Recovered Solvent Chemical
Price 60 INR/ Kilograms
MOQ : 100 Kilograms
Recovered Solvent Chemical Specification
- Purity
- 99.99%
- Form
- Liquid
- Grade
- Industrial Grade
- Type
- Recovered Solvent
- Physical State
- Liquid
- Packaging Type
- Barrel
- Shelf Life
- 2 Years
- Packaging Size
- 160 Kg
Recovered Solvent Chemical Trade Information
- Minimum Order Quantity
- 100 Kilograms
- Payment Terms
- Cash in Advance (CID)
- Supply Ability
- 5000 Kilograms Per Month
- Delivery Time
- 2-7 Days
- Main Domestic Market
- All India
About Recovered Solvent Chemical
Discover exceptional value with this Recovered Solvent Chemical, now available at a reduced price for a limited time-last chance to personalise your bulk orders! Sourced and supplied by a noble and meritorious trader in India, this industrial-grade recovered solvent boasts a 99.99% purity, a substantial 2-year shelf life, and comes in convenient 160 Kg barrels. Ideal for various industrial applications, its liquid form guarantees versatility and efficiency for your site's operations. Secure this opportunity for cost-effective and environmentally responsible chemical solutions today!
Diverse Applications & Machine Features of Recovered Solvent Chemical
Recovered Solvent Chemical is utilised in numerous sectors, including pharmaceuticals, paint manufacturing, adhesives, and cleaning industries. It is particularly advantageous at sites where solvent recovery machines are in use, maximising efficiency and sustainability. Key features of using advanced recovery machines include consistent purity levels, reduced waste, and improved environmental compliance, making this product suitable for rigorous industrial demands.
Export Markets & Logistics Solutions for Recovered Solvent Chemical
Our Recovered Solvent Chemical serves main export markets across Asia and Europe, while also catering to India's robust domestic market. Express shipping and reliable transport services ensure timely delivery, with samples available upon request for quality assurance. Customers are encouraged to inquire about the asking price and benefit from flexible purchasing options, meeting their specific needs for industrial-grade solvents efficiently.
Diverse Applications & Machine Features of Recovered Solvent Chemical
Recovered Solvent Chemical is utilised in numerous sectors, including pharmaceuticals, paint manufacturing, adhesives, and cleaning industries. It is particularly advantageous at sites where solvent recovery machines are in use, maximising efficiency and sustainability. Key features of using advanced recovery machines include consistent purity levels, reduced waste, and improved environmental compliance, making this product suitable for rigorous industrial demands.
Export Markets & Logistics Solutions for Recovered Solvent Chemical
Our Recovered Solvent Chemical serves main export markets across Asia and Europe, while also catering to India's robust domestic market. Express shipping and reliable transport services ensure timely delivery, with samples available upon request for quality assurance. Customers are encouraged to inquire about the asking price and benefit from flexible purchasing options, meeting their specific needs for industrial-grade solvents efficiently.
FAQ's of Recovered Solvent Chemical:
Q: How is the Recovered Solvent Chemical typically used in industry?
A: Recovered Solvent Chemical is commonly utilised for cleaning, degreasing, and as a raw material in manufacturing processes within industries like pharmaceuticals, paints, and chemicals.Q: What is the purity and shelf life of this recovered solvent?
A: This industrial-grade recovered solvent boasts a high purity of 99.99% and offers a reliable shelf life of 2 years, ensuring optimal performance during storage and use.Q: Where can I apply this recovered solvent chemical?
A: It is suitable for use in facilities employing solvent recovery systems, as well as in applications requiring high-purity solvents, such as manufacturing plants, cleaning units, and laboratories.Q: What are the packaging options for this product?
A: The recovered solvent is available in sturdy 160 Kg barrels, making it convenient and safe for storage and large-scale industrial use.Q: Is sample availability and express shipping offered?
A: Yes, samples are available upon request to verify quality. We offer express shipping and efficient transport services to both domestic and main export markets.Q: How can I personalise my order or inquire about the asking price?
A: You can personalise your order by contacting our supplier team in India, who will provide detailed information on current pricing and available package specifications.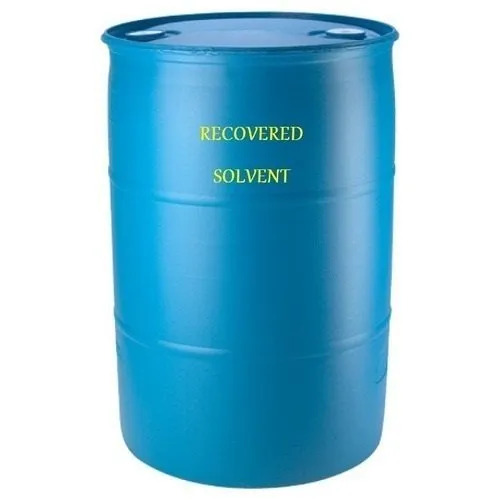
Tell us about your requirement

Price:
Quantity
Select Unit
- 50
- 100
- 200
- 250
- 500
- 1000+
Additional detail
Mobile number
Email

More Products in Industrial Solvent Chemical Category
Melamine Powder
Price 81 INR / Kilograms
Minimum Order Quantity : 100 Kilograms
Molecular Formula : C3H6N6
Purity : >99%
Form : Powder
Boiling point : Not applicable (decomposes)
Tri Ethyl Amine Chemical
Price 150 INR / Kilograms
Minimum Order Quantity : 100 Kilograms
Molecular Formula : C6H15N
Purity : 99.99%
Form : Liquid
Boiling point : 89 Degree C
Methylene Dichloride Chemical
Price 40 INR / Kilograms
Minimum Order Quantity : 100 Kilograms
Molecular Formula : CH2Cl2
Purity : 99.99%
Form : Liquid
Boiling point : 39.6 Deg C
N Heptane Chemical
Price 118 INR / Kilograms
Minimum Order Quantity : 100 Kilograms
Molecular Formula : C7H16
Purity : >99.9%
Form : Liquid
Boiling point : 98.4C

Contact Details
Mangaldeep Chemical
GST : 27ALEPP8997Q1ZQ
- Parwati Apt, 1st Floor, Office No.6, Uthalsar Naka, Thane West,Thane - 400003, Maharashtra, India
 Send Inquiry

Developed and Managed by Infocom Network Private Limited.
